Views: 0 Author: Site Editor Publish Time: 2026-09-22 Origin: Site


Elevator Traction Belts have transformed the elevator industry by providing a more efficient, reliable, and sustainable alternative to traditional elevator systems that rely on wire ropes. As technology advances, the demand for quieter, more energy-efficient, and cost-effective elevator solutions increases. Elevator Traction Belts meet these demands and more, offering several advantages over conventional systems.
In this article, we will dive deeper into the key benefits of Elevator Traction Belts, how they outperform wire ropes, and why they have become the preferred choice in modern elevator designs. These belts provide building owners and operators with an innovative, long-lasting solution that improves performance, reduces maintenance, and enhances the passenger experience.
One of the most compelling reasons to choose Elevator Traction Belts is their longer service life. Traditional wire ropes often experience wear and tear due to their design, requiring regular maintenance, lubrication, and eventual replacement. Elevator Traction Belts, on the other hand, are built to last significantly longer, reducing the frequency of replacements and lowering long-term maintenance costs.
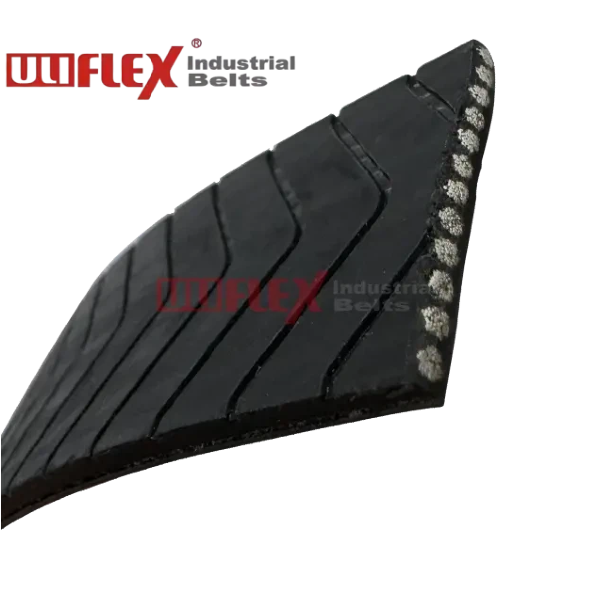
The steel cord encapsulation within Elevator Traction Belts provides robust reinforcement, helping them maintain their strength and structural integrity under heavy loads and constant tension. This design protects the belts from abrasion and environmental damage, which are common issues faced by wire ropes. Additionally, the polyurethane (PU) coating that encapsulates the steel cords provides an extra layer of protection, extending the lifespan of the belts and ensuring consistent performance.
Due to their superior durability, Elevator Traction Belts require less frequent replacement compared to traditional wire ropes. Building owners can save on both replacement costs and the labor required to install new ropes. Over time, this results in a lower overall lifecycle cost for the elevator system.
Furthermore, the extended service life of Elevator Traction Belts means fewer service interruptions, reducing the downtime of the elevator system and ensuring continuous operation, especially in high-rise buildings or commercial complexes that rely on elevators for frequent traffic.
One of the most noticeable benefits of Elevator Traction Belts is their ability to reduce noise and vibration during operation. Traditional wire ropes tend to produce more noise and cause vibrations as they move over the drive sheave, which can be disruptive in residential and commercial buildings. In contrast, Elevator Traction Belts offer a smoother ride with significantly less noise and vibration.
The smooth operation of the Elevator Traction Belt reduces the mechanical friction and tension that would otherwise cause vibrations and noise. This feature is especially important in buildings with residential apartments, hotels, or offices where quiet operation is a priority. Passengers in elevators equipped with Elevator Traction Belts enjoy a more comfortable and peaceful ride, free from the rattling or buzzing noises typical of older elevator systems.
By eliminating these noises, Elevator Traction Belts enhance the overall passenger experience. Building owners who prioritize comfort and convenience for tenants or visitors will find that these belts offer substantial advantages over traditional wire ropes.
Additionally, because Elevator Traction Belts produce fewer vibrations, they are less likely to damage the elevator components over time. This leads to a reduction in wear and tear on other parts of the elevator system, further extending the lifespan of the equipment and reducing the need for costly repairs.
As urban spaces become more densely populated and high-rise buildings continue to rise, maximizing the use of available space has become increasingly important. Elevator Traction Belts contribute to space efficiency by enabling more compact elevator designs. Traditional wire ropes require large sheaves and extensive motor assemblies, making them less suitable for space-constrained environments. In contrast, Elevator Traction Belts are much smaller in size, allowing for the design of machine-room-less (MRL) elevators that save both space and cost.
In machine-room-less (MRL) systems, the motor and drive sheave are integrated into the elevator shaft itself, eliminating the need for a separate machine room. This innovation not only saves valuable space in high-rise buildings but also reduces construction and operational costs. Elevator Traction Belts are a critical component in making MRL systems a reality, as their compact design allows for the efficient use of available space.
Additionally, Elevator Traction Belts offer installation efficiency. Their design makes them easier to install and maintain compared to wire ropes. The reduction in the need for large, cumbersome machinery means that the installation process is quicker and less costly. The compact size of the belts also allows for easier retrofitting of older elevator systems, making them ideal for buildings undergoing upgrades or renovations.
Table: Advantages Overview
Advantage |
What It Means to You |
Long lifespan |
Lower lifecycle cost |
Quiet ride |
Better user experience |
Compact |
Design flexibility |
Less maintenance |
Lower upkeep cost |
As shown in the table above, Elevator Traction Belts offer a variety of benefits that not only improve the performance of the elevator system but also save money in the long run. The long lifespan and reduced maintenance requirements lower the total cost of ownership, while the quiet ride and compact design enhance passenger satisfaction and space efficiency.
Energy efficiency is a key concern in modern building designs, and Elevator Traction Belts help address this challenge. These belts have a high friction coefficient that allows them to transfer torque from the motor to the elevator car with minimal energy loss. In traditional systems using wire ropes, a significant amount of energy is lost due to slippage between the rope and the drive sheave. This results in higher energy consumption and increased operational costs.
With Elevator Traction Belts, less energy is lost to friction, making the system more efficient. This reduction in energy consumption is particularly beneficial in high-rise buildings or commercial properties that rely on multiple elevator systems to serve large numbers of people. The energy efficiency of Elevator Traction Belts can contribute to lower electricity bills and help meet green building standards, such as LEED (Leadership in Energy and Environmental Design) certifications.
As building codes continue to emphasize sustainability and energy-saving solutions, Elevator Traction Belts are increasingly becoming the standard for modern elevator systems. By reducing energy waste and improving overall efficiency, they contribute to more environmentally friendly and cost-effective building operations.
Safety is paramount in any elevator system, and Elevator Traction Belts offer enhanced safety and reliability compared to traditional wire ropes. The even stress distribution provided by the steel cord reinforcement within the belts ensures that the load is consistently balanced, reducing the risk of sudden failures or malfunctions. This balanced load distribution helps minimize the chances of wear and tear, ensuring that the elevator operates smoothly and safely over its lifespan.
Elevator Traction Belts also feature built-in redundancy and engineering safety margins, which ensure the continued operation of the system even if one part of the belt system experiences a fault. This redundancy provides an extra layer of security for passengers and minimizes the risk of accidents or breakdowns.
Because of the durable and reliable design of Elevator Traction Belts, they are particularly suited for buildings where safety is a top priority. The belts’ ability to handle heavy loads, resist wear, and function effectively over extended periods of time makes them an excellent choice for both low-rise and high-rise elevators.
The Elevator Traction Belt offers numerous advantages over traditional wire rope systems, making it the preferred choice for modern elevator systems. From its longer service life and lower maintenance costs to its quiet ride and space-saving design, the Elevator Traction Belt delivers superior performance that benefits both building owners and passengers alike.
Whether you are installing a new elevator system or upgrading an existing one, Elevator Traction Belts from Uliflex provide the reliability, cost-effectiveness, and energy efficiency needed for modern buildings. With their advanced design and operational benefits,high-quality Elevator Traction Belts help create a smoother, more efficient elevator system while reducing overall costs and enhancing passenger comfort. For more information or to discuss your project needs, please contact us today.
What makes Elevator Traction Belts more energy-efficient than traditional wire ropes?
Elevator Traction Belts have a high friction coefficient that allows them to transfer more torque with minimal energy loss, resulting in lower energy consumption and reduced operational costs.
How do Elevator Traction Belts improve ride comfort?
The Elevator Traction Belt reduces vibrations and noise, providing a smoother and quieter ride compared to traditional wire ropes, enhancing the overall passenger experience.
Are Elevator Traction Belts suitable for all types of elevators?
Yes, Elevator Traction Belts are versatile and suitable for various elevator systems, including residential, commercial, and machine-room-less (MRL) systems.
How long do Elevator Traction Belts last compared to wire ropes?
Elevator Traction Belts typically last up to 15 years, significantly longer than wire ropes, which need more frequent maintenance and replacements.